
SCHUNK's TRIBOS polygonal clamping technology for micro-machining
 InfoWeb Marketplace · Editorial team
Published on 9 October 2013 · 5 min read
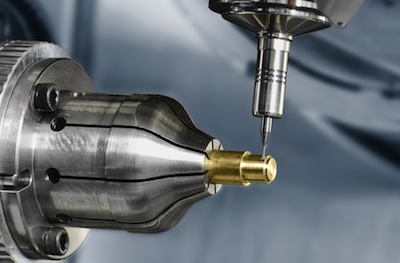
Maintaining machining tolerances of a few micrometers requires clamping devices with perfect concentricity. What seems obvious becomes a long-term challenge when, for example, the initial precision of the tool seat deteriorates over time, or is not achieved repeatably because of minimal variations.
It was following similar problems with various clamping devices that the Swiss manufacture Chopard, a watchmaking specialist, decided to replace its micro-machining toolholders with SCHUNK's TRIBOS polygonal clamping technology. Since then, process stability has improved markedly.
Chopard's watches are a skilful blend of design, ultramodern technology and traditional craftsmanship. The prestigious L.U.C movements are entirely designed and produced within the Chopard manufacture. Even the gold used is cast by Chopard according to specific alloys. All models are developed in-house, and the employees' know-how and technical expertise are invaluable. Nine movement families offered in more than fifty variants are the best proof of this.
Tests prove very high reliability in micro-machining.
The long manual work of Chopard's experienced watchmakers is based on high-precision parts from their own machining workshop. Two totally independent teams are responsible for machining the watch cases: one team for parts in stainless steel or titanium and one for parts in gold, cases and bracelets.
Machining steel parts is closer to series production, whereas working with gold is more like small-batch production. For Richard Hiltbrunner, head of industrial development, and Franck Rosnowski, programmer and head of cutting tools, the investment in new production equipment was an ideal starting point to reorganize the internal processes and optimize them according to the demands of the different materials. Every toolholder was put through testing.
?Before the reorganization, we used collets,? explains Richard Hiltbrunner. ?Whenever there was a machining inaccuracy, the question arose whether the problem came from the spindle, the toolholder or the tool.? The micro-machining specialists tested various toolholders on a new turn-mill center 508 MT from Willemin Macodel, with an HSK-E interface 40.
SCHUNK's TRIBOS polygonal clamping technology proved to be the most reliable clamping method. ?Since we have been using TRIBOS, the spindle and toolholder form a rigid, extremely safe and reliable unit,? confirms Franck Rosnowski.
Maintenance-free, wear-free clamping
With a concentricity and repeatability of less than 0,003 mm, measured at a tool projection length of 2,5 x D and a balancing quality of G 2.5 at 25.000 tr/min, TRIBOS polygonal clamping technology meets the highest requirements. The absence of moving parts makes it insensitive to mechanical wear and guarantees almost maintenance-free clamping.
Continuous tests at SCHUNK also prove that after thousands of repeated clamping cycles, no material fatigue appears, and concentricity and torque also remain perfect over time. The system is therefore far superior to other clamping technologies. The high-precision toolholders, compatible with HSM (high-speed machining), are suitable for all tool shanks of quality h6 and, depending on the type, tested up to 205.000 tr/min.
?Furthermore, changing tools is much simpler, safer and faster with TRIBOS than with other systems.? At Chopard, TRIBOS demonstrates its strengths in machining small gold batches, in the order of 20 to 200 pieces, thanks to its great flexibility. For each new setup, the machine's complete set of tools is changed. Day after day, an average of 50 toolholders have to be re-equipped, estimates Franck Rosnowski.
Using the shrink-fit unit used for mounting the toolholders, precise pressure is applied to the high-precision TRIBOS toolholders so that the polygonal bore of the toolholder becomes cylindrical. In this state, the tool can be easily inserted into the toolholder. Since the procedure takes place within a deformation limit of Rp 0,2 %, there is no plastic deformation of the steel.
When the external pressure is removed, the inner diameter returns to its initial polygon shape owing to the elasticity of the material, and the residual stress in the steel holds the tool by friction. Since the chuck does not expand in length during the opening procedure, it is guaranteed that tools can be set with a length tolerance of 0,01 mm. This is an advantage over thermal shrink fitting, because the tool length is reduced as the toolholder cools.
Process reliability and flexibility
For the manufacture of watches bearing the highly prized ?Poinçon de Genève? quality label, Chopard now uses more than one hundred TRIBOS polygonal clamping toolholders in its Geneva workshops. These high-precision toolholders are used for machining watch cases and prototypes in precious metals. ?While TRIBOS is used in our Fleurier workshops mainly for its high precision, in Geneva it is the flexibility, process reliability and surface quality achieved that are emphasized,? explains Franck Rosnowski.
To obtain very thin walls and sometimes very complex parts, TRIBOS's vibration damping is very valuable, especially for machining gold, since the surface finish of the machined parts is paramount. Because of the rigidity and flexibility of the process, the clamping system is also used for machining steel parts. ?We can no longer do without it, whether in prototype production or in series machining where high geometric demands are made,? says Franck Rosnowski.
Special variants for milling and drilling
Chopard uses SCHUNK polygonal clamping toolholders for clamping shank diameters of 3, 4, 6 and 10 mm. The smallest cutting diameter is 0,08 mm. Chopard uses the TRIBOS-RM, dedicated to precision milling, in a high speed range of up to 85.000 tr/min. This toolholder offers high radial rigidity, which allows the capabilities of HSM machining centers to be fully exploited.
Its clamping force allows large chip removal depths with excellent concentricity. Thanks to its polygonal design, the TRIBOS-RM absorbs vibrations, thus contributing to longer tool life and a flawless surface finish. With HSK-A interfaces 25, 32, 40, HSK-E 25, 32, 40, HSK-F 32, BT 30 and SK 30, the TRIBOS-RM is perfectly suited to the needs of machining centers.
For drilling applications, Chopard uses the TRIBOS-Mini, dedicated to very high-precision work. With the TRIBOS-Mini, designed for rotation speeds of up to 205.000 tr/min, all calibrated tool shanks h6 can be clamped, starting from a diameter of 0,3 mm. TRIBOS-Mini is available for HSK-A interfaces 25, 32, 40, HSK-E 20, 25, 32, 40, HSK-F 32, BT 30 and SK 30. For tool changes, Chopard uses several shrink-fit units of types SVP-2D and SVP-2. TRIBOS polygonal clamping technology is one of the most comprehensive programs for high-precision tool clamping. The high-precision toolholders are manufactured exclusively at SCHUNK's headquarters in Lauffen am Neckar, Germany.